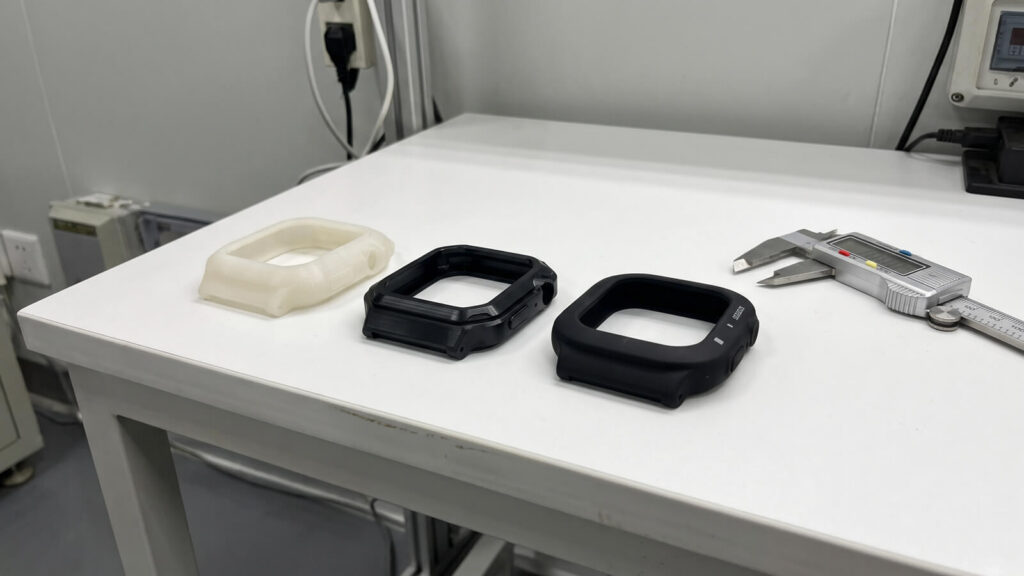

For hardware startups, mid-sized consumer brands, and mechanical engineers, transitioning a product from a 3D CAD file to retail-ready inventory hinges on one core manufacturing discipline: custom plastic injection molding. When launching high-value accessories retailing above $30—such as multi-layer rugged smartphone cases, industrial VR/AR headset housings, graded trading card slab protectors, or child-resistant enclosures—injection molding delivers the tight dimensional repeatability (±0.01mm), surface finish versatility, and unit economics that 3D printing and CNC machining cannot match at scale.
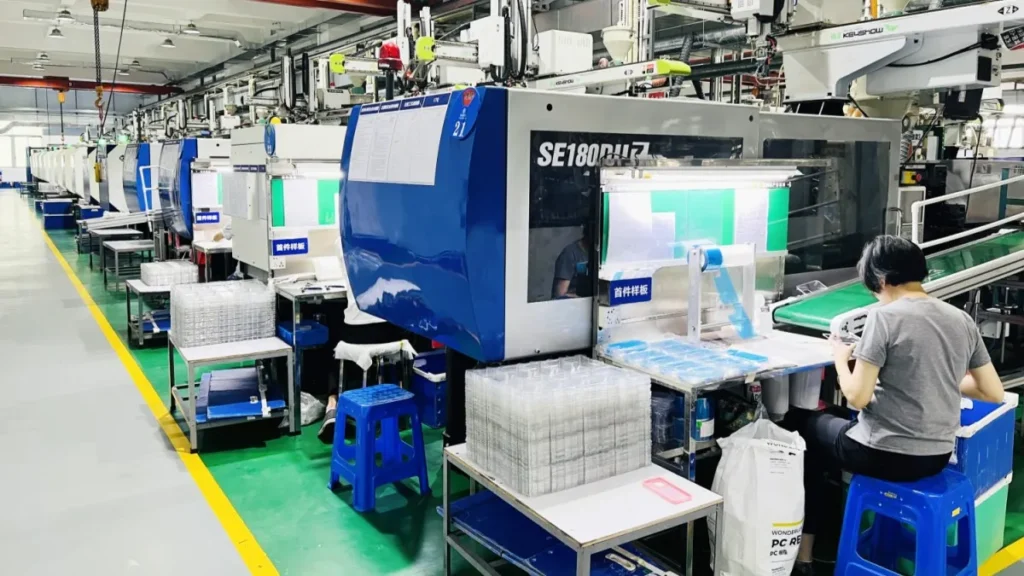
Drawing from our operational experience across 130+ injection molding presses since 1996, this engineering breakdown walks through press mechanics, precision mold making, the six-stage scientific molding cycle, and how modern bridge tooling lowers the barrier to entry for agile product teams.
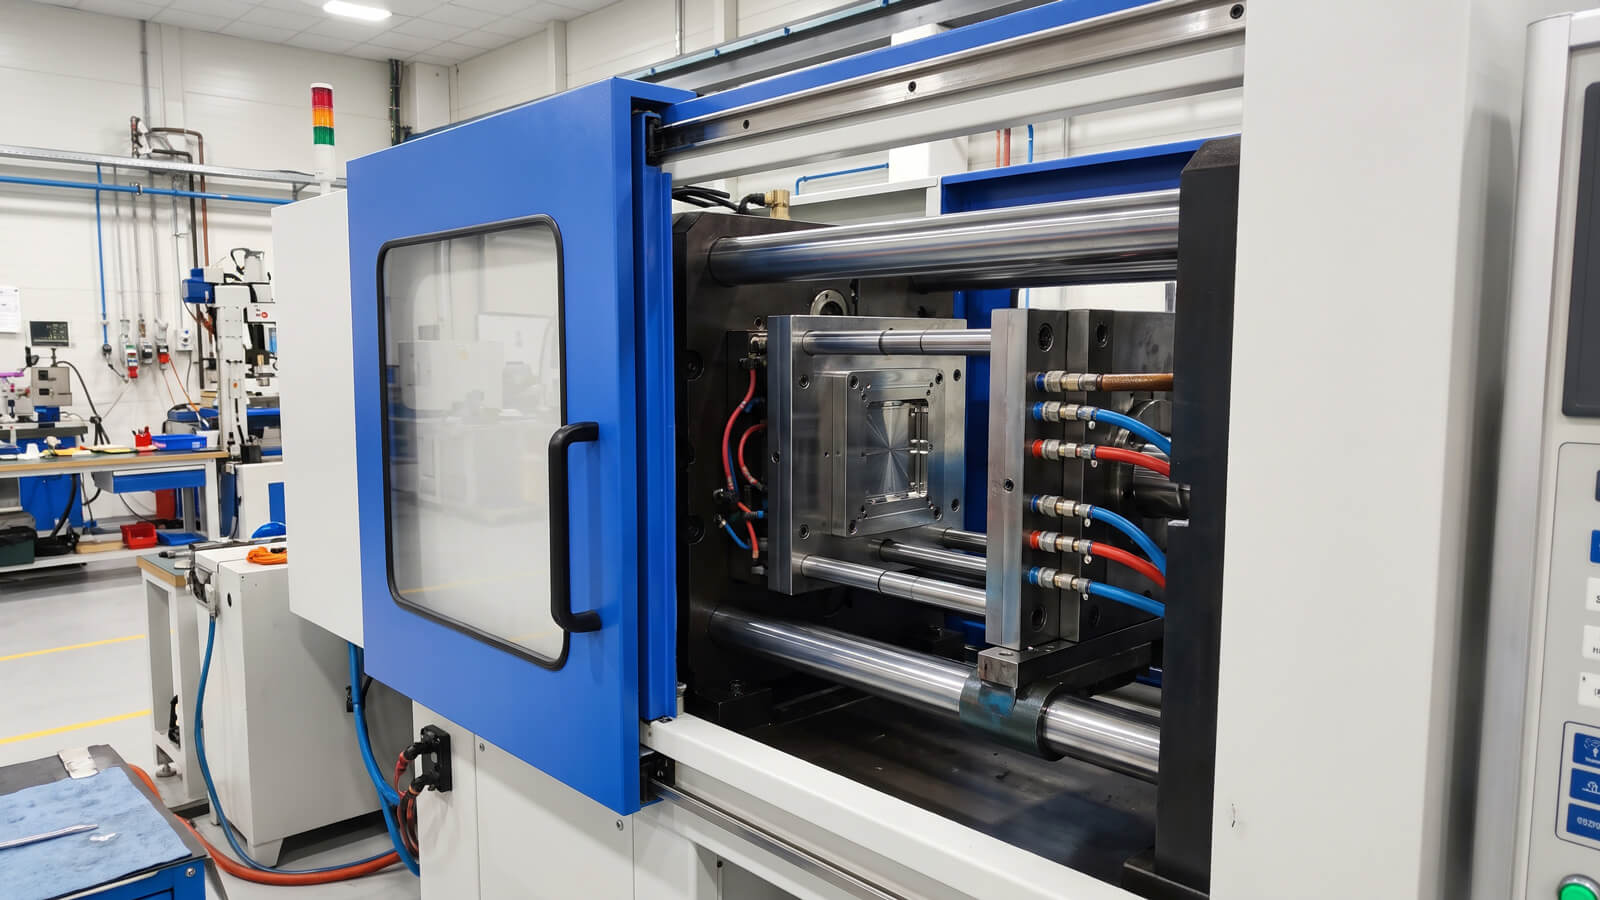
What Is Injection Molding & How Does the Machine Work?
At its core, plastic injection molding services convert solid thermoplastic pellets or liquid elastomers into complex, net-shape components through controlled heat and high-pressure injection. Inside an injection press (spanning 50T to 800T of clamping force at YG TECH), four primary hardware subsystems work in sequence:
Stores and feeds pre-dried polymer resin pellets directly into the feed throat without ambient moisture exposure.
Uses multi-zone PID heater bands and shear friction to melt engineering plastics (PC, ABS, PA, PPS) to an exact melt viscosity.
Rotates to homogenize the melt and acts as a high-velocity hydraulic or servo-electric ram to inject resin through the nozzle.
Two mating halves (Core and Cavity) held shut under tonnage while internal cooling lines solidify the part prior to pin ejection.
Phase I: Injection Mold Design & Precision Tool Manufacturing
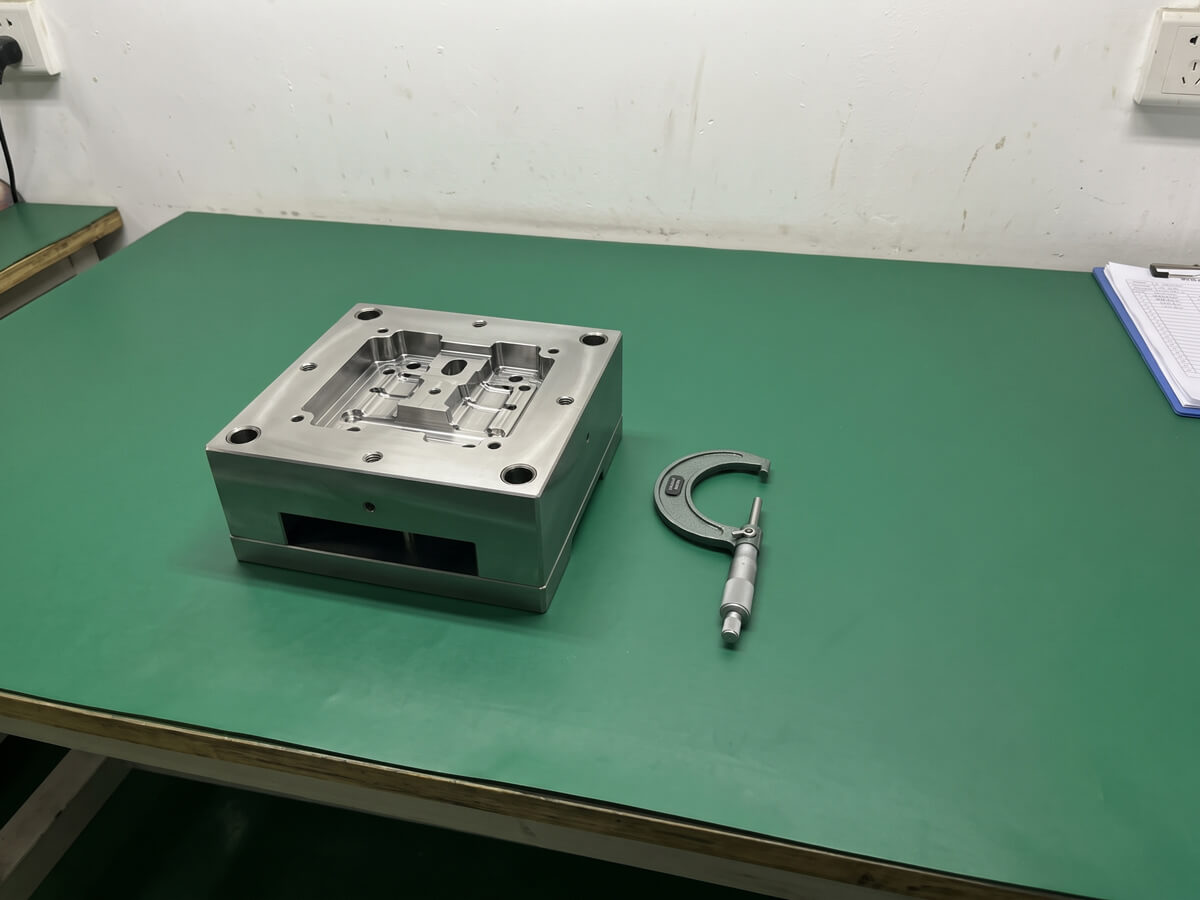
A molded part is only as accurate as the steel cavity that forms it. Before production begins, every project passes through three structured injection mold manufacturing milestones:
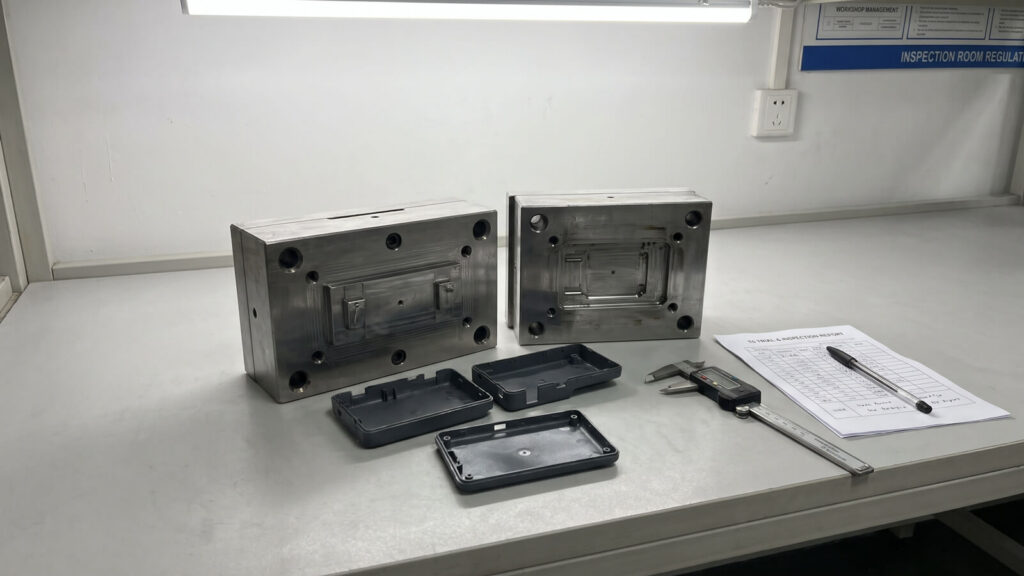
- DFM & Mold CAD Engineering: Under an upfront NDA, our engineers audit your 3D part geometry for uniform wall thickness, draft angles (1.5°–3°), parting line placement, submarine or hot-runner gate positioning, and ejector pin balance.
- Tool Steel Selection & Micron Machining: While soft aluminum tools quickly wear out, we machine hardened tool steels (such as S136, H13, and NAK80) to a standard tolerance of ±0.01mm—and down to ±0.002mm on shut-offs—using 5-axis CNC milling, mirror Sinker EDM, and slow-feed Wire EDM. For startups and SMEs seeking lower upfront capital risk, our MUD (Master Unit Die) rapid tooling services use shared master frames to cut mold costs by 30% and deliver T0 samples in as fast as 10 days, while dedicated production molds carry a 300,000 to 500,000-shot lifespan.
- T0 Mold Trial & Scientific Optimization: During initial mold trials, engineers balance cavity fill rates, verify VDI 3400 or SPI optical surface finishes, and inspect first-article samples on 3D CMM and 2.5D vision systems.
Phase II: The 6-Stage Injection Molding Production Cycle
Once the mold is approved for production, executing repeatable injection molding process steps relies on tight thermal and pressure control across six continuous stages (Source: Society of Plastics Engineers):
Upload your 3D STEP file under an upfront NDA. Our MUD rapid tooling system cuts mold costs by 30% and delivers T0 molded parts in as fast as 10 days.
High-Value Application Niches & Advanced Molding Technologies
Rather than competing in low-margin commodity housewares or heavy automotive bumpers, YG TECH engineers specialized tooling and cleanroom molding exclusively for high-value plastic accessories retailing above $30. We pair standard thermoplastics with advanced processes—including LSR/LIM (Liquid Silicone Rubber), 2K Two-Shot Overmolding, IMD (In-Mold Decoration), and IM-3D-E (In-Mold 3D Electronics)—across four core sectors:
| Target Niche Sector | Representative $30+ Accessory Products | Key Resins & YG TECH Process Advantage |
|---|---|---|
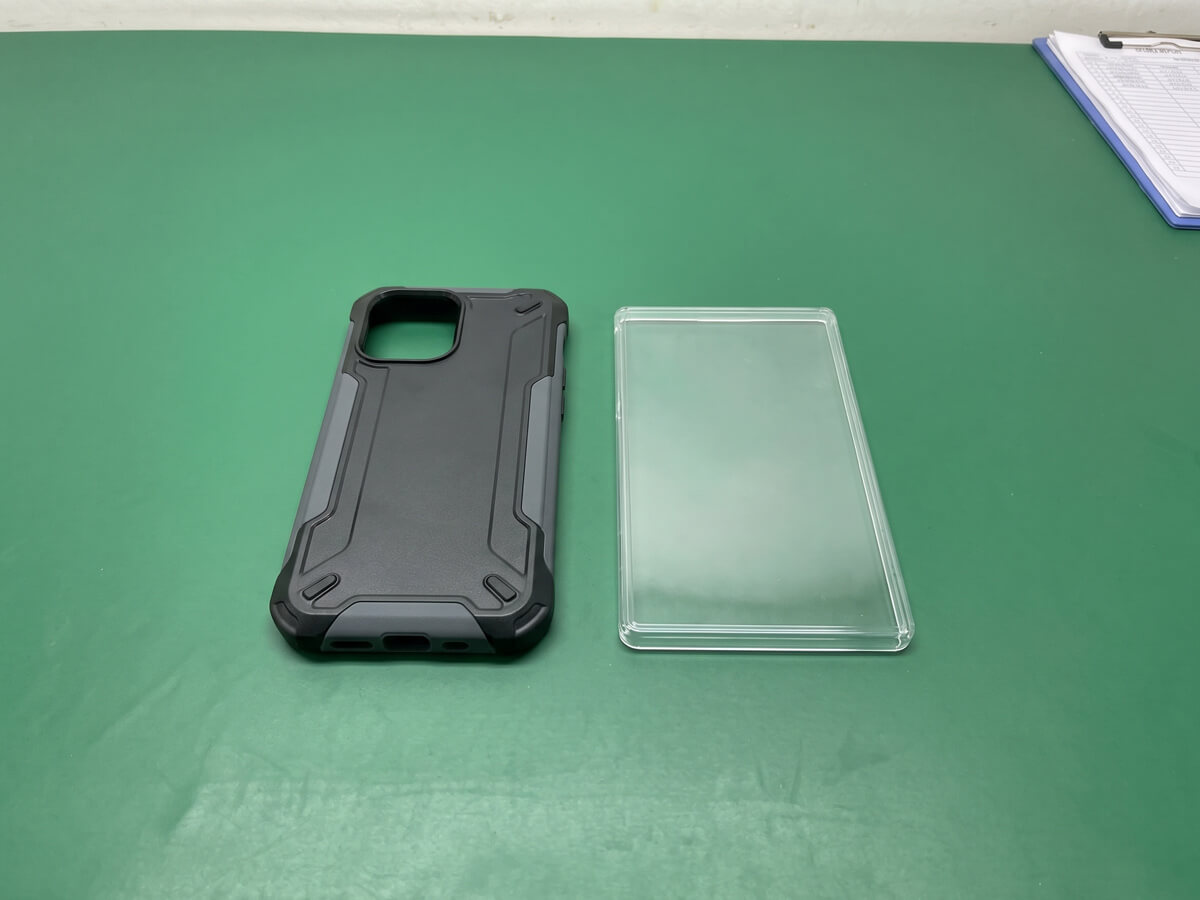
| Consumer Electronics & Peripherals | Multi-layer MagSafe / rugged phone cases, 68/98-key mechanical keyboard frames | PC + TPU 2K overmolding, PBT keycaps, scratch-proof IMD foils, simple PCBA drop-in assembly. |
| Spatial Computing & Industrial AR/VR | VR/AR headset structural visors, optical sensor mounts, LSR facial cushions | Glass-filled PA, specialty high-temp PPS, and skin-safe LSR molded in an ISO Class 8 cleanroom. |
| Collectible & High-Net-Worth Protection | PSA trading card slab protectors, display cases for sneakers & art figurines | UV-stabilized optical PC (Ra < 0.05 μm mirror polish) with shock-absorbing elastomer bumpers. |
| Specialty & Medical-Grade Enclosures | Child-resistant lock boxes, diagnostic handheld shells, smart air purifier housings | Backed by ISO 13485, ISO 9001, RoHS, and GRS 4.0 certified recycled resin traceability. |
Future Trends: GRS Circular Polymers & Smart In-Mold Integration
Global supply chains are rapidly shifting toward sustainable materials and consolidated electronics packaging (Source: Plastics News). At YG TECH, we help Western SMEs stay ahead of retail compliance through two proven capabilities:
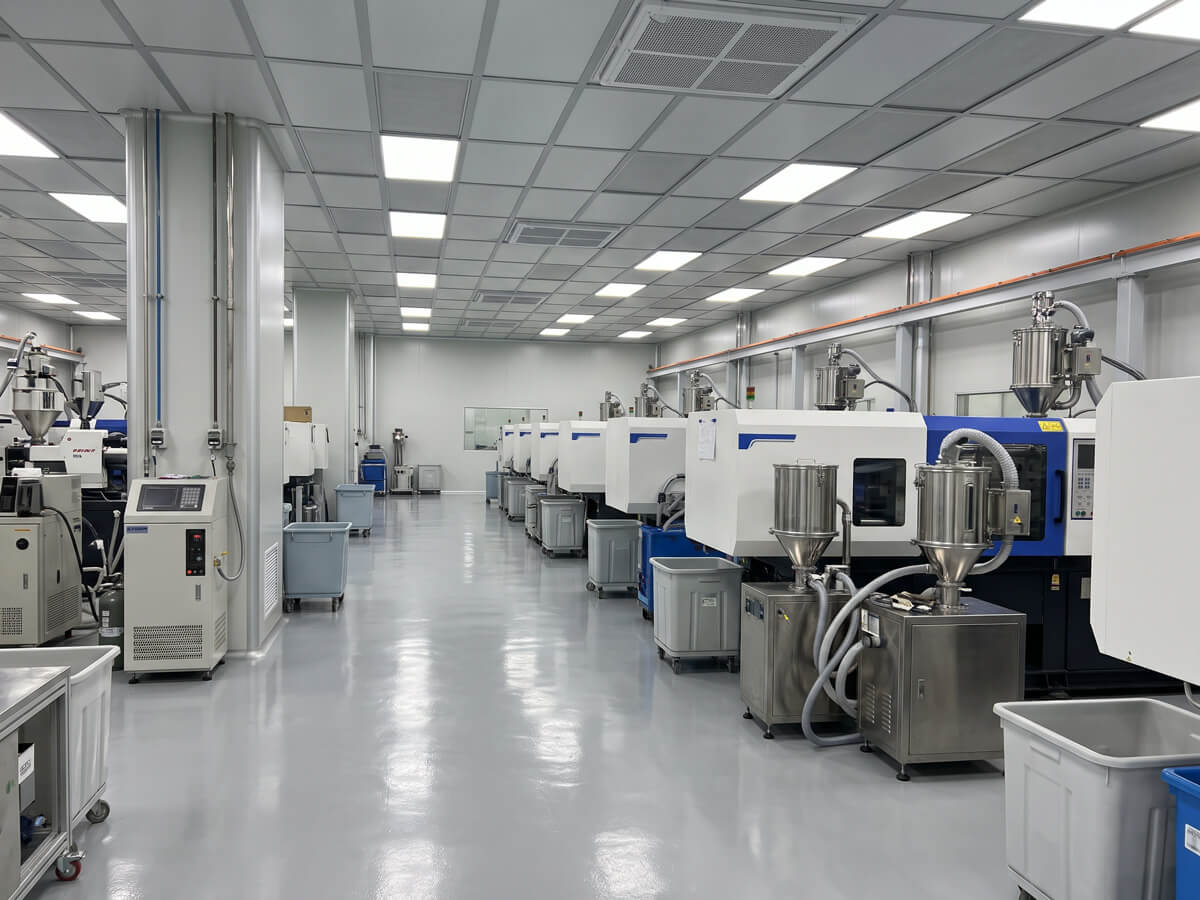
- GRS 4.0 Certified Recycled Plastics & All-Electric Presses: Certified to ISO 14001 and GRS 4.0 (Global Recycled Standard) and audited by both Amazon and Walmart, we process Post-Consumer Recycled (PCR) polycarbonate, ABS, and TPU on energy-efficient servo-electric presses with closed-loop runner recycling.
- Rapid Prototyping to Bridge-Tooling Continuity: By combining 3D printing and CNC prototyping with IM-3D-E (embedding touch circuits or simple PCBA assemblies directly inside the molded shell), brands eliminate secondary assembly vendors and accelerate time-to-market.
Debunking Injection Molding Myths & Buyer FAQs
Engineering Reality: With MUD rapid tooling (-30% mold cost) and our startup-friendly 1,000-piece standard MOQ, custom molding often beats 3D printing on unit cost and mechanical strength starting at just 500 to 1,000 parts.
Engineering Reality: At YG TECH, we sign an upfront NDA and guarantee in writing that 100% of the mold ownership transfers unconditionally to the client upon full payment.
Q1: How long is the typical injection molding cycle and tooling lead time?
Press cycle times range from 12 to 45 seconds per shot depending on wall thickness. For tooling, our MUD rapid tooling delivers T0 samples in as fast as 10 days, while standard hardened production molds take 25 to 35 days.
Q2: How do you handle quality defects if a batch falls out of spec?
Rather than brushing off issues with blind part replacements, we execute a closed-loop quality resolution process: tracing resin batch certificates, reviewing scientific molding logs, verifying dimensions via CMM, and performing steel-safe mold corrections collaboratively.
Q3: What payment and shipping terms do you support for Western SMEs?
We recommend hassle-free EXW or door-to-door DDP delivery to the US, UK, Canada, Europe, and Australia, paired with flexible payment terms covering 100% upfront for rapid samples, standard 50% deposit, or Net 30 credit terms for qualified recurring partners.
Ready to Launch Your Custom Plastic Accessory Project?
Send us your 3D CAD files (STEP/IGES) for a free engineering DFM review, resin recommendation, and a transparent quote comparing 10-day MUD rapid tooling vs. mass-production steel molds.