
When hardware startups and mid-sized brands look to reduce custom plastic injection molding costs, the first instinct is often commercial negotiation—pushing suppliers to shave a few cents off their profit margin. Yet in precision manufacturing, supplier margins represent only a tiny fraction of your landed unit price. Nearly 80% of a molded part’s total cost is locked in by engineering choices: mold architecture, wall thickness geometry, runner scrap ratios, press tonnage pairing, and post-molding assembly labor.
For sourcing managers and product engineers launching high-value accessories retailing above $30—such as multi-layer rugged smartphone cases, industrial VR/AR headset frames, crystal-clear trading card slab protectors, and child-resistant storage enclosures—cutting costs can never come at the expense of cosmetic yield or drop-test durability. Below is a practical engineering framework Drawn from nearly three decades of production experience at YG TECH, showing how to systematically strip waste out of both upfront tooling capital (CapEx) and recurring unit production (OpEx).
What Actually Determines the Cost of Injection Molding?
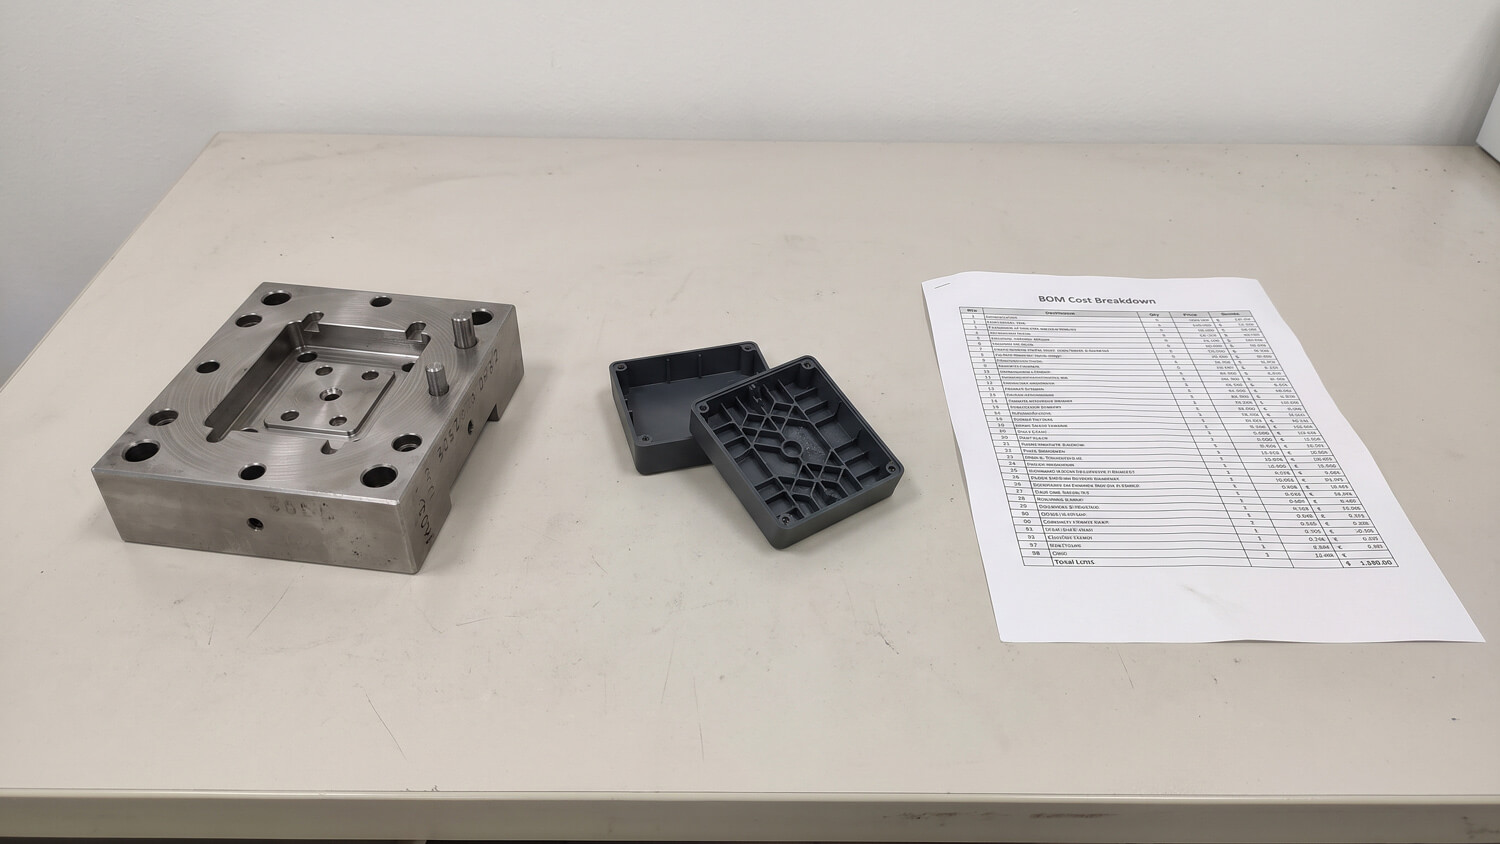
Before pulling specific cost-reduction levers, you must understand how a contract manufacturer calculates your part quote. Whether you are ordering a 1,000-unit pilot batch or scaling to 100,000+ units via plastic injection molding services, total landed cost is governed by four interlocking drivers:
1. Cut Upfront Tooling Costs by 30% Using MUD Rapid Tooling & CAE Moldflow
For emerging brands and SMEs, mold amortization is often the biggest barrier to profitability. If you spend $18,000 on a conventional multi-plate steel mold to produce an initial batch of 2,000 protective cases, tooling amortization alone adds $9.00 to every single unit before a gram of plastic is injected. Understanding how much an injection mold costs—and how to restructure that investment—is your most powerful early-stage cost lever.
Deploy MUD (Master Unit Die) Shared Mold Frames for Pilot & Bridge Runs
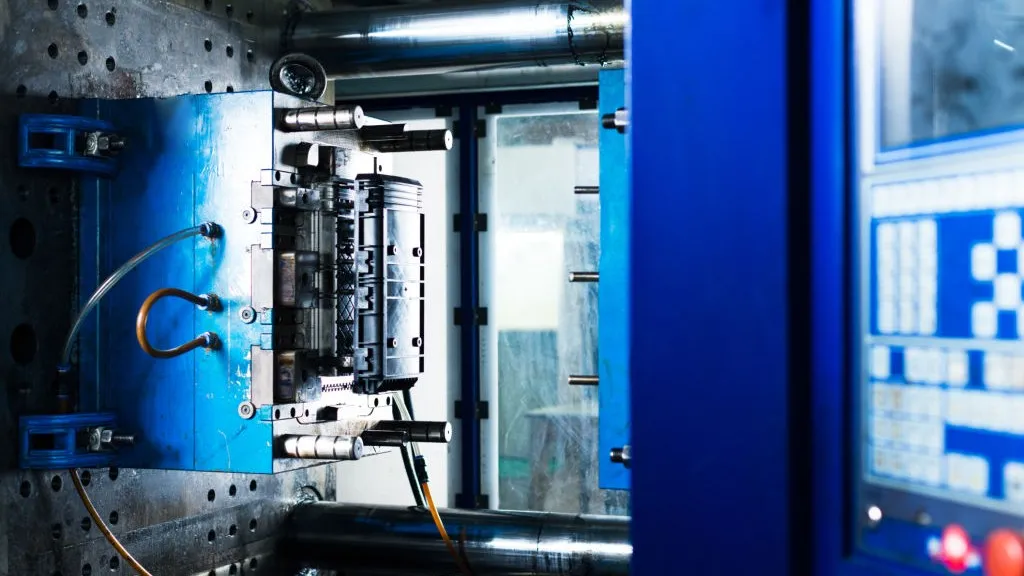
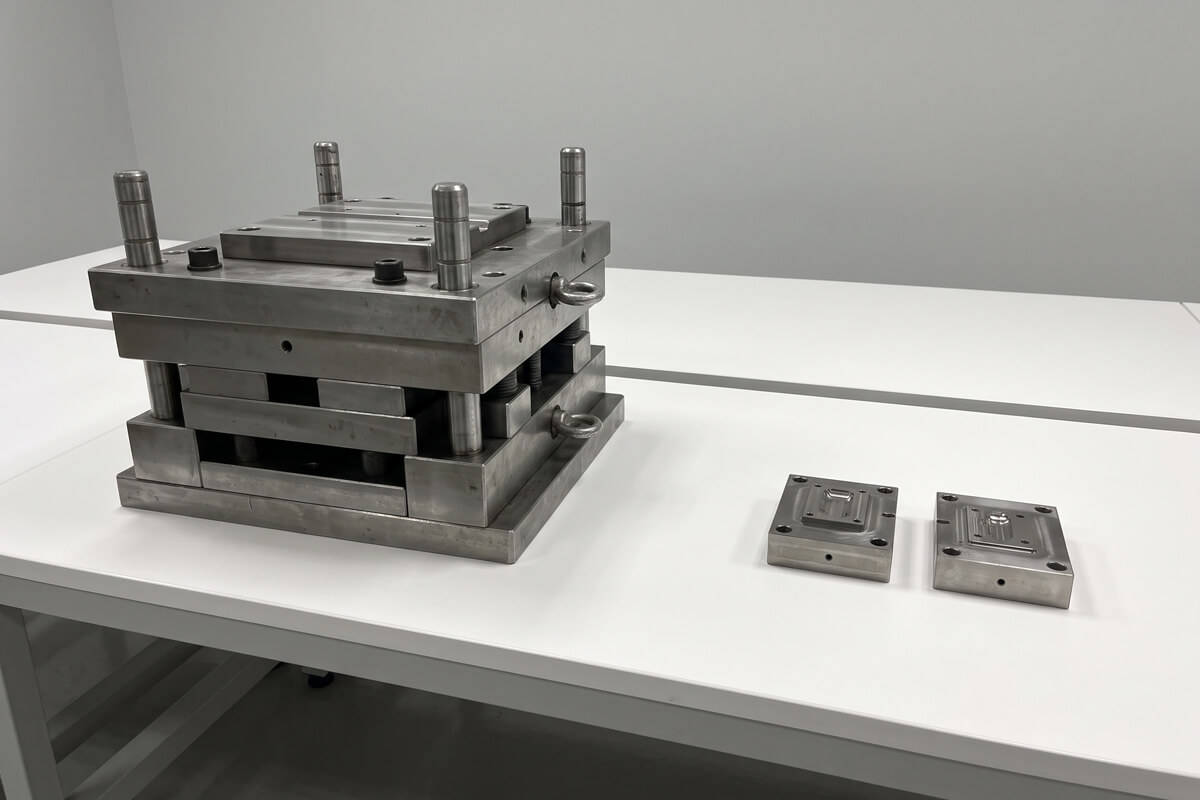
In a traditional standalone mold, nearly 35% to 40% of the tooling invoice goes toward purchasing and machining the heavy outer steel mold base (A-plate, B-plate, ejector housing, and clamping plates). Through our rapid tooling services, we eliminate that redundant expense using a MUD (Master Unit Die) quick-change system. Because YG TECH maintains pre-engineered master mold frames on the press floor, you only pay to machine the custom core and cavity inserts specific to your part geometry. This lowers upfront tooling costs by up to 30% and compresses lead times so you receive production-grade T0 samples in as fast as 10 days.
Eliminate Steel Rework with Upfront CAE Moldflow Simulation
Trial-and-error mold debugging wastes both machine hours and engineering budgets. Before cutting hardened steel, our engineers run Computer-Aided Engineering (CAE) Moldflow simulations on every project. By virtually testing gate locations, filling balance, shear stress, and cooling shrinkage, we catch air traps, weld lines on snap-fit hooks, and warpage tendencies on screen—reducing physical mold trials from three or four rounds down to T0/T1 approval.
2. DFM Part Optimization: Wall Coring, Draft Angles, and Undercut Elimination
Small geometric adjustments made during Design for Manufacturability (DFM) yield compounding savings across every single shot for the life of the tool:
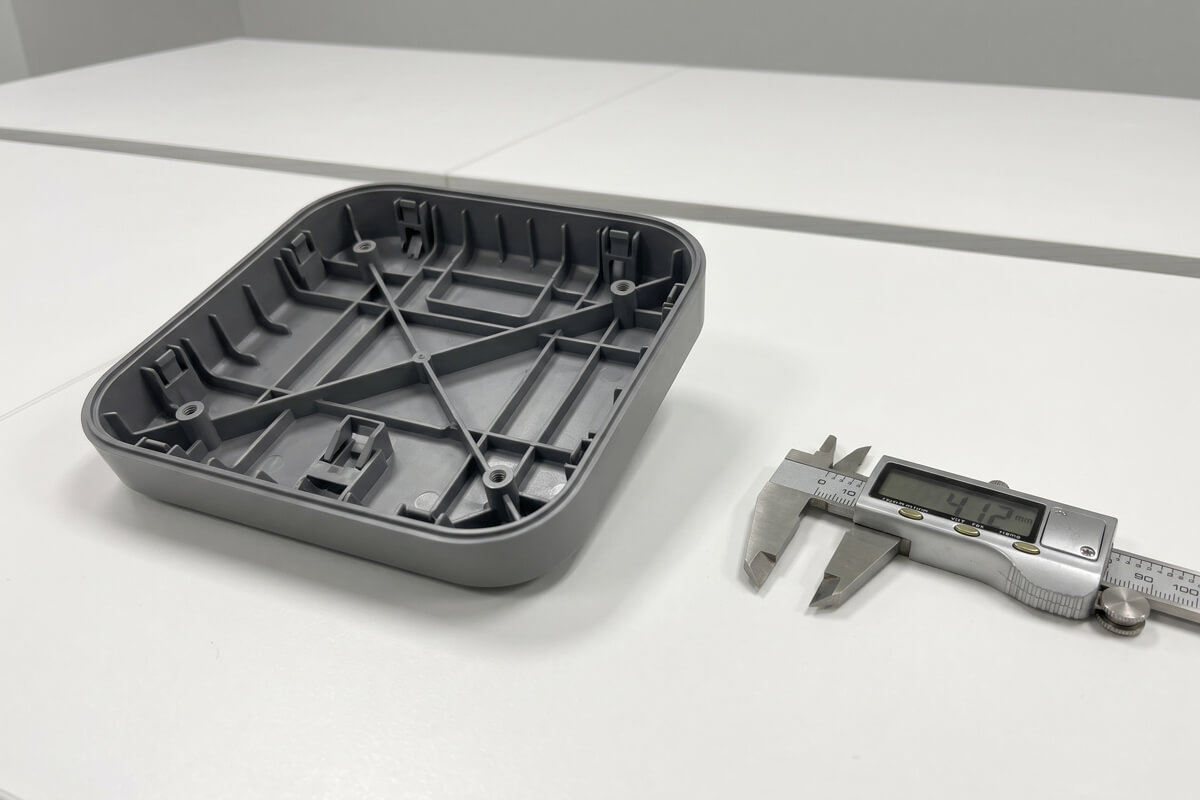
- Core Out Thick Sections (“Uniform Wall Shelling”): Plastic cooling time is proportional to the square of the wall thickness (Source: Plastics Technology). Doubling a housing wall from 2.0mm to 4.0mm does not double cooling time—it quadruples it! By hollowing out solid bosses and replacing thick walls with a uniform 1.8mm–2.2mm shell supported by 1.0mm reinforcing ribs, you simultaneously reduce resin weight by 20%–35%, eliminate cosmetic sink marks, and cut press cycle time in half.
- Replace Mechanical Side-Sliders with “Pass-Through” Shut-Offs: Every external side-action slider or internal angled lifter adds $800 to $2,500+ to the mold price and requires slower press open/close speeds. Where cosmetically acceptable on internal B-surfaces, redesigning side snap hooks with a “pass-through” window allows the core and cavity to form the undercut directly along the vertical line of draw—eliminating moving sliders entirely.
- Specify Functional Draft & Relax Non-Critical Tolerances: While YG TECH routinely holds ±0.01mm mold tolerances (and ±0.002mm on slow-feed Wire EDM shut-offs), applying ultra-tight tolerances to every non-mating exterior curve forces unnecessary EDM and CMM inspection hours. Apply tight tolerances strictly to PCBA mounting datums, optical lens seats, and sealing perimeters, while giving vertical walls a generous 1.5° to 2.5° draft angle so parts eject smoothly without cycle-slowing ejection delays.
3. Right-Size Press Tonnage (50T–800T) and Leverage All-Electric Efficiency
In factory operations, one of the most expensive hidden markups passed onto buyers is press tonnage mismatch—often referred to by mold engineers as “using a racehorse to pull a handcart.”
Every injection molding machine has an hourly operating rate based on its clamping force, footprint, and power draw. If you contract with a small job shop that only owns 350-ton and 500-ton hydraulic presses, they will run your small 60-ton wearable housing mold on a 350-ton machine. Not only do you end up paying a 350-ton machine-hour rate on every part, but running a small shot volume inside an oversized screw barrel leads to excessive polymer residence time—causing thermal yellowing in clear polycarbonate and material degradation in heat-sensitive resins.
| Accessory Category & Projected Area | Optimal Clamping Tonnage Tier | Cost Penalty of Oversized Press | YG TECH Fleet Advantage (130+ Presses) |
|---|---|---|---|
| Precision Clips, Keycaps, Small Bezels (< 25 cm²) | 50T – 90T High-Speed Presses | +35% to +60% machine-hour markup if run on 250T+ | Fast dry-cycle speeds; minimal barrel residence time. |
| Phone Cases, PSA Card Protectors (60–150 cm²) | 120T – 250T Precision / Cleanroom Presses | +25% to +40% cost penalty + optical yellowing risk | Paired with ISO Class 8 cleanroom & rotary 2K units. |
| VR/AR Headsets, 68/98-Key Keyboards (180–350 cm²) | 280T – 450T Servo-Hydraulic / Hybrid | Under-tonnage causes flash; over-tonnage inflates rate | Balanced platen rigidity for zero-warpage long frames. |
| Multi-Cavity Storage Boxes & Purifier Shells (> 400 cm²) | 500T – 800T High-Tonnage Presses | Requires high-flow screw plasticizing capacity | Supports large family molds & high-cavitation output. |
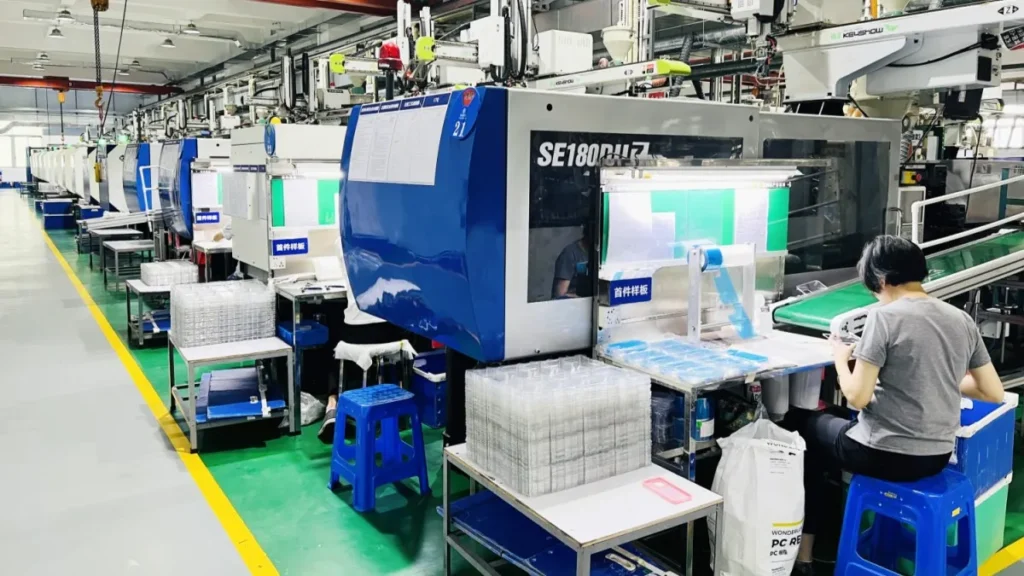
Because YG TECH operates 130+ high-end injection molding machines spanning 50T to 800T—including all-electric and servo-hybrid machines that consume 20% to 80% less energy than legacy fixed-pump hydraulic presses (Source: Plastics Industry Association)—we match your tool to the exact clamping tonnage and barrel shot size required, keeping your machine-hour rate lean.
4. Runner Architecture & Conformal Cooling: Compressing Cycle Seconds
Once your mold is mounted in the right press, unit cost is dictated by two numbers: how much plastic is wasted per shot, and how many seconds the press takes to cycle.
Hot Runner vs. Cold Runner Break-Even Analysis
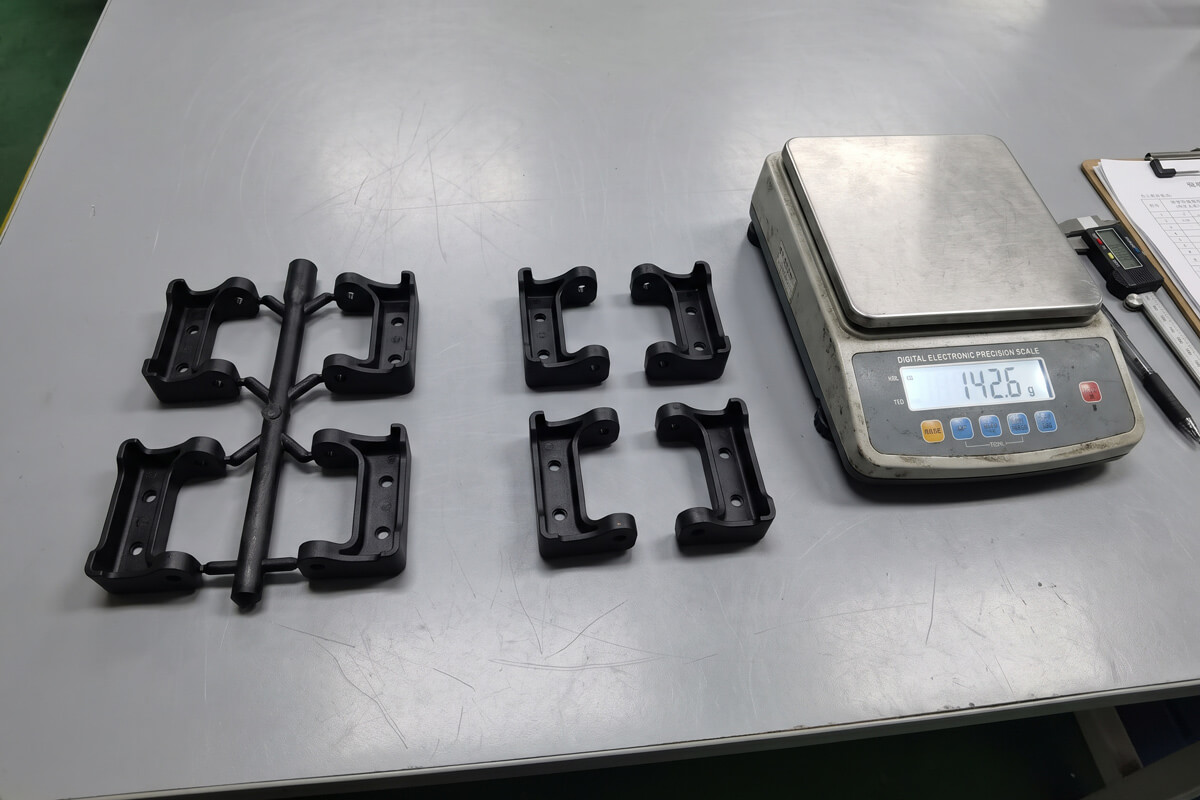
In a standard cold-runner mold, the solidified plastic inside the sprue and runner channels is ejected alongside the parts. If you are molding small, lightweight accessories out of expensive specialty resins—such as high-temperature PPS (Polyphenylene Sulfide), optical-grade polycarbonate (where regrind cannot be mixed back in without hurting optical clarity), or platinum-cured LSR—cold runner scrap can easily exceed 30% to 50% of your raw material bill.
By upgrading to hot runner injection molding, heated manifold nozzles inject molten plastic directly into the part cavity with zero runner scrap. Moreover, because the mold does not have to wait for a thick central sprue to solidify, a hot runner system typically shortens overall cycle time by 15% to 25%. During DFM, our engineers calculate the exact order volume where resin and cycle-time savings fully pay back the upfront hot-runner manifold investment.
Fast-Cooling Inserts & Scientific Molding Parameter Preservation
Cooling absorbs 60% to 75% of the entire injection molding cycle. In deep cores—such as tall protective case walls or deep cylindrical enclosures—conventional straight-drilled water channels cannot reach the tip of the steel core, creating localized hot spots that force operators to extend cooling timers. We eliminate these thermal bottlenecks by integrating high-conductivity beryllium-copper / Moldmax sub-inserts and baffled conformal cooling circuits directly beneath heat-intensive geometry.
Equally important for SMEs ordering recurring batches of 1,000 to 5,000 units is digital process parameter preservation. Every time a mold is pulled from storage and re-mounted in a press, traditional “trial-and-error” setup wastes hours of machine time and dozens of startup scrap shots. At YG TECH, once a scientific molding window is validated at T1, every parameter—barrel zone temperatures, multi-stage injection velocity, V/P switchover point, holding pressure curve, and mold chiller flow rate—is digitally archived in the machine controller and linked to the tool’s barcode for instant, zero-waste recall on future reorders.
Send us your 3D STEP file or existing part specs under an upfront NDA. Our engineers will calculate your exact savings across MUD rapid tooling (-30% CapEx), wall coring, and hot-runner break-even volume.
5. Consolidate Post-Molding Labor via In-Mold Technologies (2K, IMD & IM-3D-E)
Every time a molded part is removed from the press and moved to a secondary workshop for painting, silk-screening, glue dispensing, or manual gasket installation, you pay for extra handling labor, work-in-progress (WIP) storage, and cumulative scrap across multiple steps. Consolidating those secondary processes directly inside the injection mold slashes total assembly cost:
Instead of molding a rigid PC shell and manually gluing on a rubber bumper or waterproof gasket, our overmolding service and LSR/LIM cells chemically bond soft TPU, TPE, or liquid silicone directly onto the substrate inside a single molding cycle—eliminating adhesive labor and delamination defects.
Post-molding spray painting and multi-pass pad printing suffer from 5%–12% dust and alignment reject rates. IMD feeds a pre-printed decorative film into the mold cavity and back-injects clear or tinted resin behind it, delivering finished, scratch-proof multi-color graphics straight out of the press.
For smart accessories containing capacitive touch buttons, LED indicators, or simple PCBA modules, IM-3D-E integrates functional circuitry directly into the structural plastic shell—reducing overall BOM part count, screw fasteners, and final assembly time by up to 40%.
6. Smart Material Management: Closed-Loop Drying and GRS 4.0 Recycled Resins
Raw polymer pellets typically represent 30% to 50% of unit production cost at scale. Controlling material cost requires disciplined resin engineering rather than buying cheap, uncertified off-grade pellets that cause field failures:
- Prevent Hydrolysis Scrap via Closed-Loop Dehumidifying Dryers: Hygroscopic engineering plastics—including polycarbonate (PC), ABS, PA66, PBT, and TPU—absorb ambient atmospheric moisture rapidly. If PC is molded with more than 0.02% moisture content, steam bubbles form silver streaks (splay) and hydrolytic chain scission destroys impact strength, turning an entire shift’s production into non-recyclable scrap. We utilize closed-loop honeycomb desiccant drying systems piped directly to the press throat to prevent moisture reabsorption and eliminate startup material waste.
- Leverage Certified GRS 4.0 Recycled Materials: Using Post-Consumer Recycled (PCR) or controlled regrind resins can lower raw material costs by 10% to 25% while satisfying corporate sustainability mandates across North America and Europe (Source: Plastics News). For internal structural frames, non-optical brackets, or matte-textured protective shells, YG TECH’s official GRS 4.0 (Global Recycled Standard) certification ensures that recycled resin blends maintain strict lot-to-lot mechanical consistency and full chain-of-custody documentation.
7. Eliminate the Hidden Cost of Poor Quality and Rigid Commercial Terms
The most expensive injection molding quote is the low-ball bid that delivers a 15% defect rate or traps your working capital in excess inventory. When evaluating total cost of ownership across your supply chain, factor in cleanroom yield and commercial flexibility:
- First-Time-Right Yield in an ISO Class 8 Cleanroom: Molding transparent collectible protectors, optical VR lenses, or light-colored LSR accessories in an open, dusty workshop results in high cosmetic reject rates due to airborne black specks—a cost the factory inevitably bakes into your unit price. Producing cosmetic-critical parts inside our ISO Class 8 cleanroom under ISO 9001, ISO 14001, ISO 13485, and RoHS quality systems (backed by Amazon and Walmart factory audits) keeps scrap rates near zero.
- Closed-Loop Quality Accountability: If a dimensional anomaly ever occurs, simply swapping defective parts without fixing the process wastes weeks of launch momentum. We enforce a strict closed-loop resolution protocol—combining resin lot traceability, CMM metrology root-cause analysis, and collaborative steel-safe mold corrections.
- Working-Capital Friendly MOQs & 100% Tool Ownership: Ordering 50,000 units just to save $0.08 per part ties up cash in warehouse storage fees. YG TECH supports a lean 1,000-piece standard MOQ, transparent EXW or door-to-door DDP delivery, and flexible payment terms (100% upfront for rapid samples, standard 50% deposit, or Net 30 credit terms for qualified recurring partners). Every project is protected by an upfront NDA, and 100% of the mold ownership transfers unconditionally to your company upon full payment—saving you from hidden “mold buyout fees” down the road.
FAQs on Injection Molding Cost Reduction
Start with functional requirements—impact resistance, UV stability, operating temperature, and optical clarity—rather than defaulting to over-specified aerospace resins. For example, switching an indoor structural bracket from expensive polycarbonate to a high-flow PC/ABS blend or GRS-certified recycled ABS can lower resin cost by 15%–25% while improving moldability and shortening cycle time.
Precision molds require CNC milling, mirror Sinker EDM, slow-feed Wire EDM, and hardened tool steels (S136/H13) built to survive 300,000 to 500,000 shots at ±0.01mm tolerances. Startups and SMEs can cut this upfront cost by up to 30%—and get T0 samples in 10 days—by using our MUD (Master Unit Die) rapid tooling system, where you only pay for custom core/cavity inserts inside a shared master frame.
Machine hourly rates are tied directly to press clamping tonnage and power consumption. Running a small mold in an oversized hydraulic press inflates your cycle cost. By matching your mold to the exact tonnage tier across our 50T–800T fleet (130+ presses) and utilizing all-electric/hybrid presses that cut energy draw by 20%–80%, we keep per-shot processing fees minimal.
Automated robotic part pickers, hot runners, and in-mold processes—such as 2K overmolding, IMD (In-Mold Decoration), and IM-3D-E—eliminate manual de-gating, secondary spray painting, and hand-gluing stations. This stabilizes cycle times to the fraction of a second, prevents human handling scratches, and consolidates multi-vendor logistics into a single turnkey shipment.
Start Your Engineering Cost-Down Audit Today
Whether you are preparing a new 3D CAD assembly for tooling or looking to reduce unit costs on an existing plastic accessory, our engineering team provides transparent, numbers-driven feedback within 24 hours: