
Ask any hardware startup founder or sourcing manager what derails a new product launch, and the answer is almost always the chasm between industrial design and toolroom reality. A concept rendering created in an external design studio may look stunning on a pitch deck. Yet the moment that 3D file reaches the mold shop, tooling engineers uncover zero-draft vertical walls, unmoldable internal undercuts, uneven wall thicknesses that guarantee sink marks, and parting lines that slice directly across high-gloss cosmetic surfaces.
Industry research consistently shows that while product design accounts for a fraction of the total development budget, decisions made during the industrial design phase lock in 70% to 80% of final manufacturing and tooling costs (Source: McKinsey & Company). For mid-sized brands and agile hardware teams developing high-value plastic accessories retailing above $30—such as rugged smartphone cases, industrial VR/AR headsets, low-profile mechanical keyboards, graded collectible slab protectors, and child-resistant enclosures—industrial design cannot exist in an artistic vacuum. It must be engineered from day one for custom plastic injection molding.
Core Principles of Industrial Design Through a Molding Engineer’s Lens
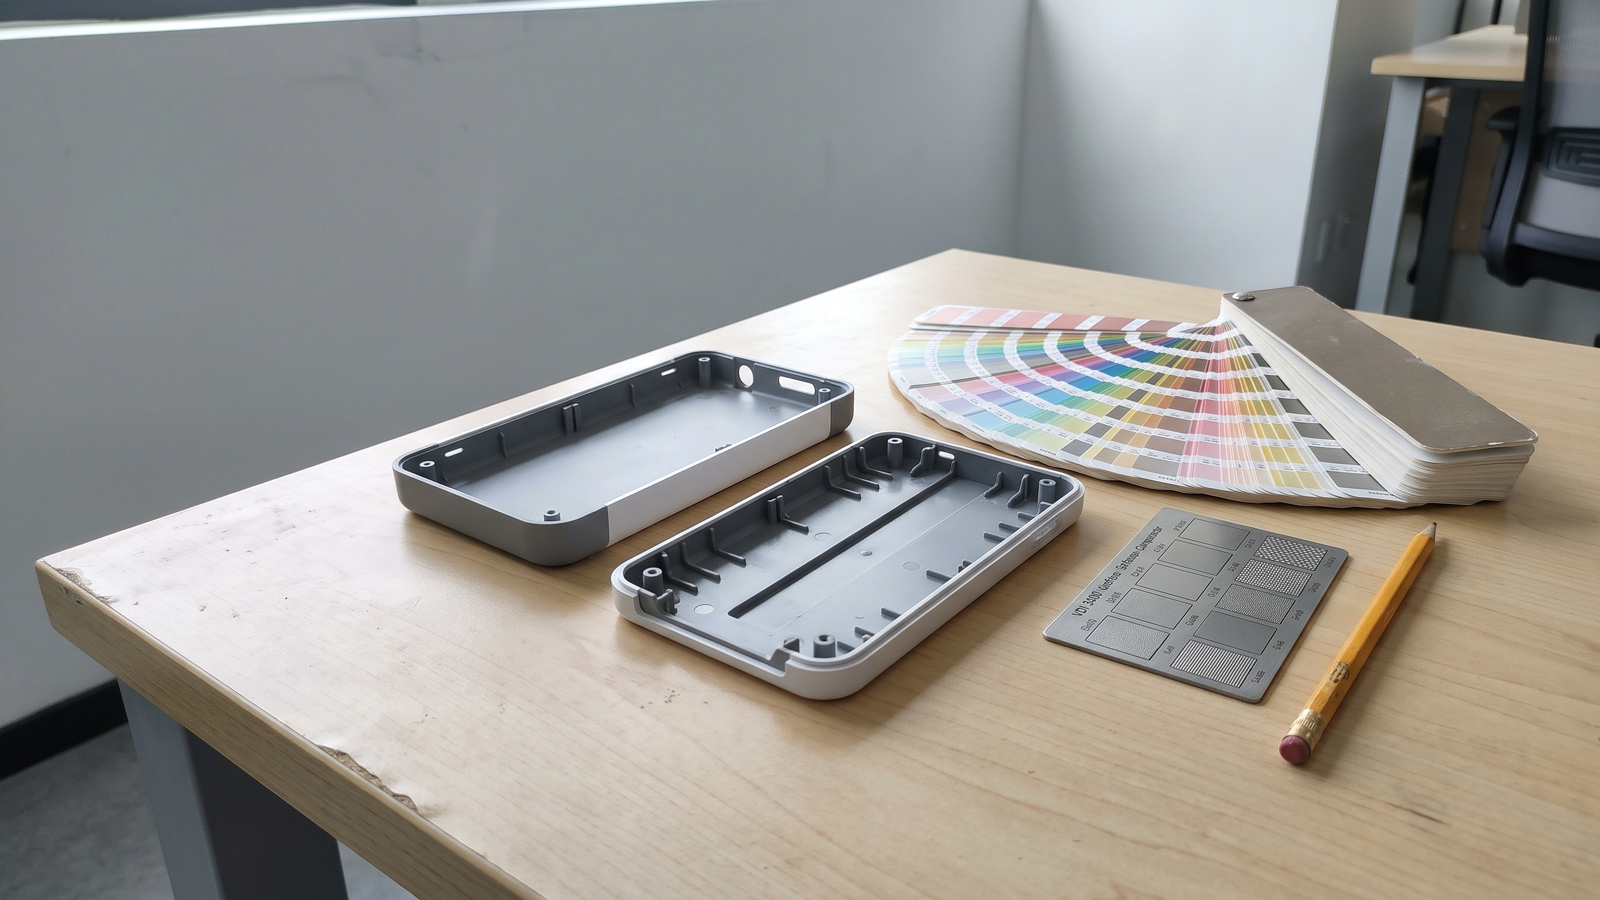
In traditional design literature, industrial design rests on three pillars: functionality, aesthetics, and ergonomics. However, when translating a 3D concept into a steel mold running at 100+ MPa of cavity pressure, our product design and tooling engineers evaluate those three principles through concrete polymer mechanics and toolmaking constraints:
A functional accessory housing must survive real-world torsion, drop impacts, and repeated snap-fit cycles without cracking or stress whitening.
Color, Material, and Finish (CMF) define brand perception on retail shelves and convey premium build quality above the $30 price point.
Ensuring physical comfort, balanced weight distribution, intuitive tactile feedback, and safety during prolonged handheld or wearable use.
The 4-Stage Industrial Design & NPI Workflow: From Concept to Steel Tooling
Turning a rough hardware idea into a shippable retail product requires a synchronized New Product Introduction (NPI) pipeline. When industrial designers and mold engineers collaborate under one roof from the start, the four classical design stages evolve from abstract theory into an agile, cost-controlled execution path:
1. Market Needs Analysis & Functional Scoping
Every successful hardware accessory begins by diagnosing specific user friction points and environmental demands. Rather than building over-complicated assemblies with high failure rates, we help SME brands strip away unnecessary mechanical complexity and focus on high-margin, high-reliability plastic structures. During this stage, our team defines target drop-test heights, UV or chemical resistance requirements, regulatory baselines (such as RoHS or child-resistant locking torque), and unit cost targets at a practical 1,000-piece minimum order quantity (MOQ).
2. Concept Design & CMF Exploration
Once functional boundaries are locked, industrial designers explore form factors, ergonomic contours, and CMF combinations through rapid 2D sketching, 3D surface studies, and photorealistic rendering. Instead of picking arbitrary colors and textures that require expensive secondary spray painting—which is prone to peeling and environmental VOC restrictions—we guide clients toward “in-mold” aesthetic solutions. These include custom masterbatch color matching, optical-grade transparent polycarbonates, dual-durometer TPU overmolding, and In-Mold Decoration (IMD) films.
3. Detailed Engineering Design & DFM Integration
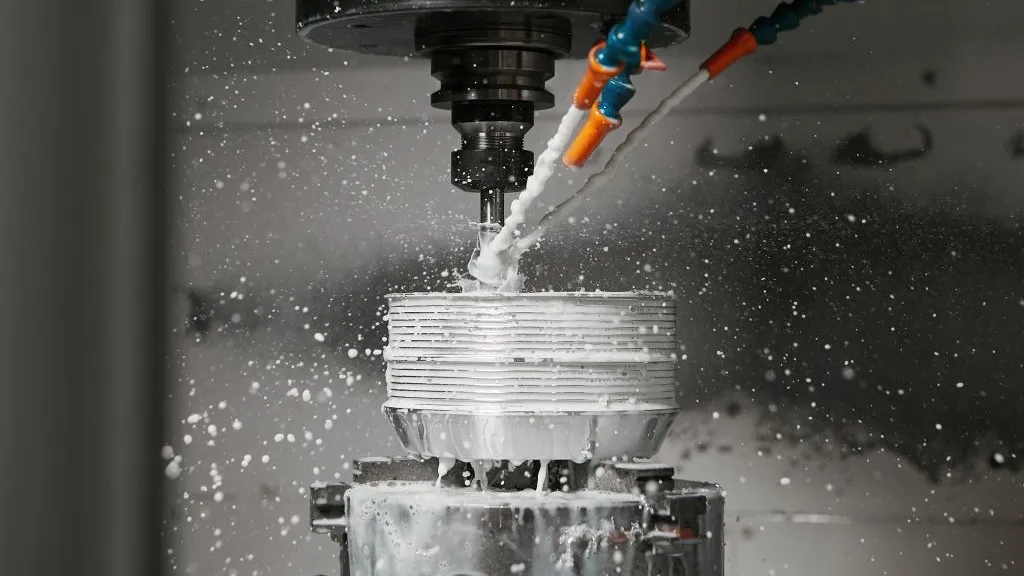
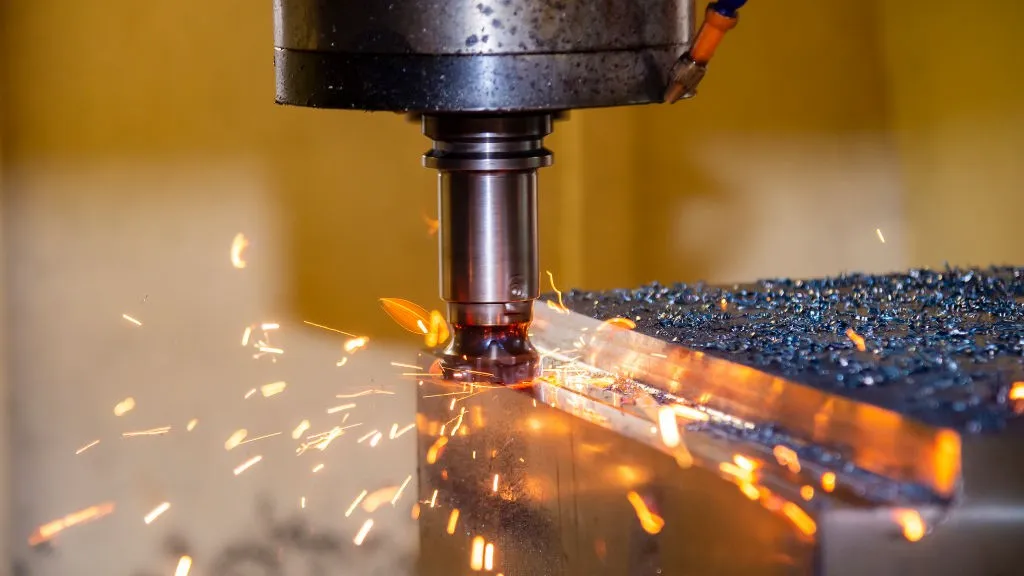
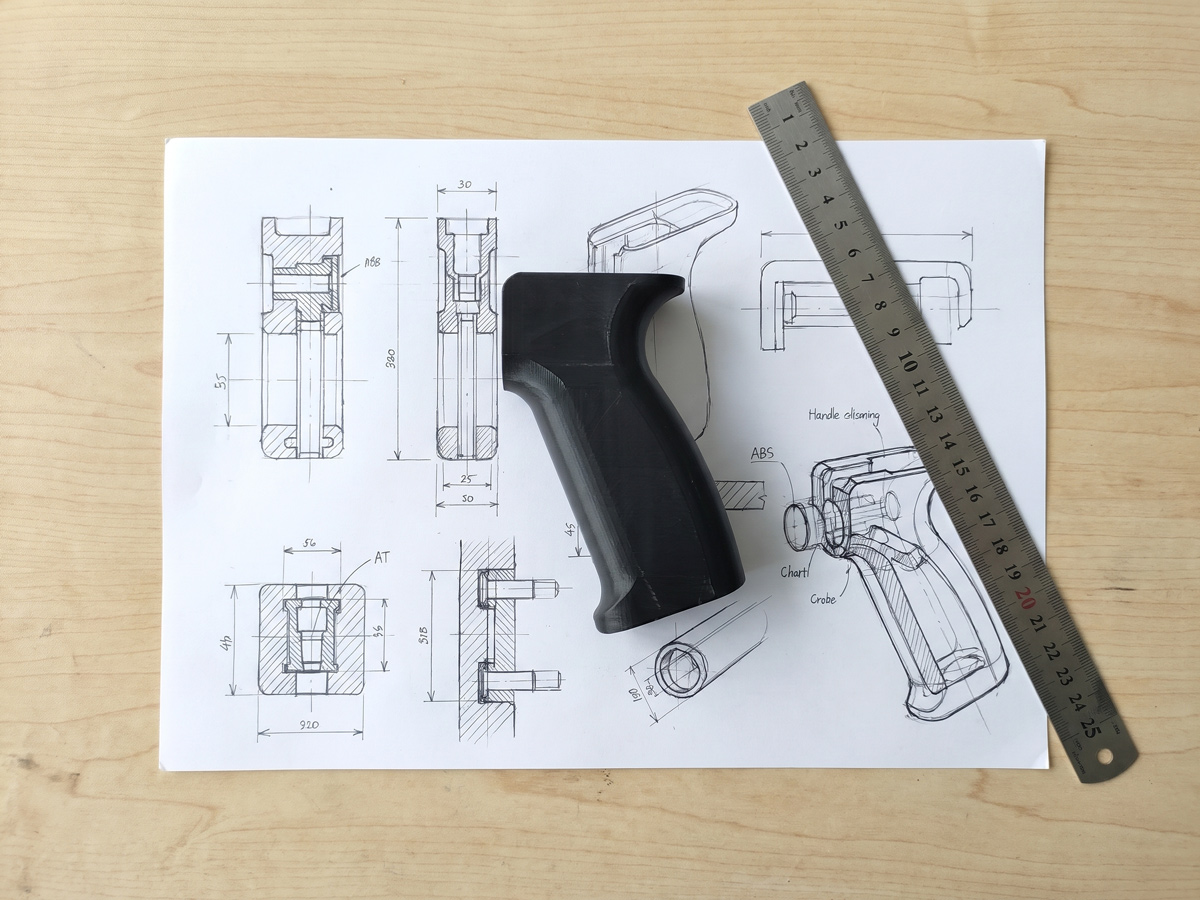
This is where most outsourced design projects stumble—and where an integrated manufacturing partner delivers the greatest value. During detailed design, aesthetic exterior shells are converted into manufacturable internal mechanics: bosses, snap hooks, ultrasonic weld energy directors, and PCBA mounting standoffs. Concurrently, our engineers verify functionality using rapid prototyping services (SLA/SLS 3D printing, CNC machining, and urethane vacuum casting) and run comprehensive Moldflow simulations to optimize gate locations and eliminate air traps before cutting steel.
4. Bridge Tooling (MUD) & Mass Production Execution
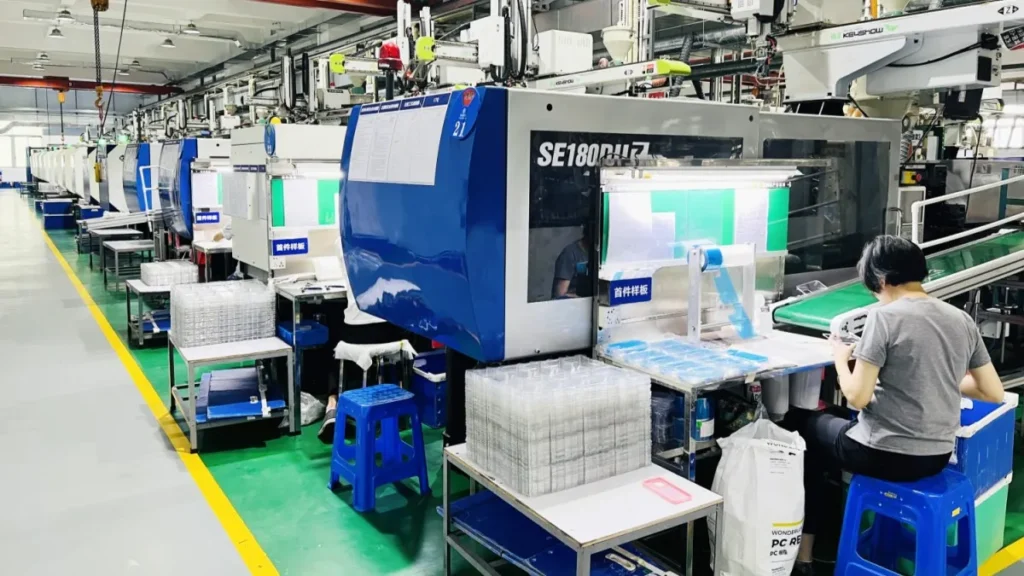
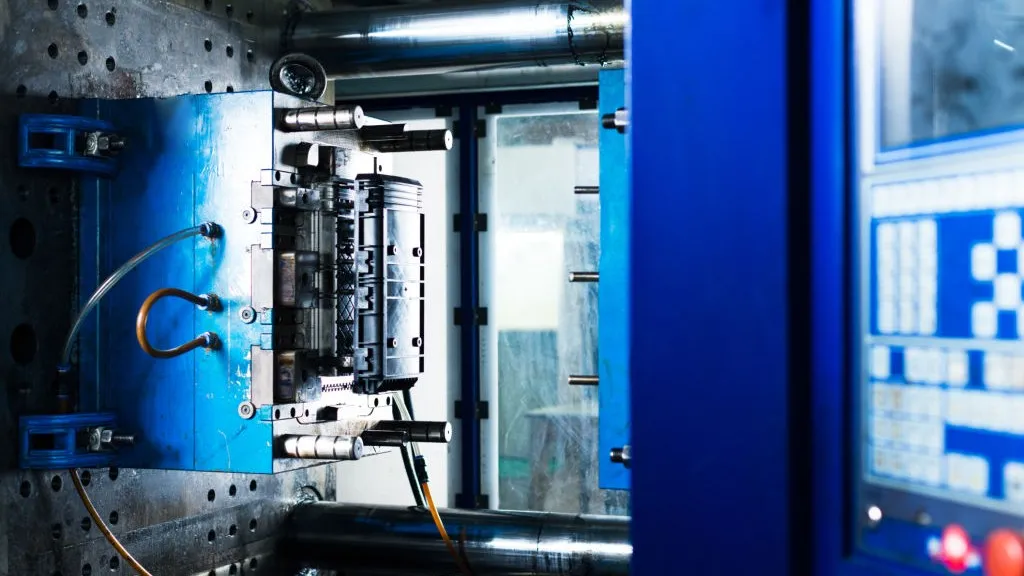
To help startups and SMEs validate market demand without locking up $50,000+ in multi-cavity production tooling, we transition detailed CAD models directly into our MUD (Master Unit Die) rapid tooling system. By machining only custom core and cavity inserts that fit inside a standardized master mold frame, our rapid tooling services cut upfront mold costs by up to 30% and deliver T0 injection-molded samples in as fast as 10 days. Once the market validates the product, we seamlessly scale into hardened S136 or H13 production molds holding ±0.01mm tolerances with a 300,000 to 500,000-shot lifespan across our fleet of 130+ injection presses (50T–800T).
The Software Toolchain: Solving the “Rhino-to-SolidWorks” CAD Handoff
A frequent pain point in hardware development stems from incompatible software workflows between industrial designers and mold makers (Source: Industrial Designers Society of America). Understanding how different software packages interact allows product teams to avoid costly CAD rebuilding fees:
When an industrial designer models a curved VR visor or ergonomic keyboard case in Rhinoceros (Rhino) and renders it in KeyShot or V-Ray, the file is often a collection of zero-thickness surfaces or non-manifold solids that cannot be directly split into a mold core and cavity. Because our engineering team works natively across both Rhino and SolidWorks, we bridge this handoff seamlessly—preserving the designer’s exact aesthetic curvature while rebuilding the internal wall thickness, parting surfaces, and ejector pin pads required for custom injection molding services.
YG TECH Industrial Design & Manufacturing Case Studies
Since 1996, we have collaborated with international hardware startups and established mid-market brands across North America, Europe, and Australia to take products from initial industrial design through cleanroom mass production. Below are four representative categories from our production portfolio:
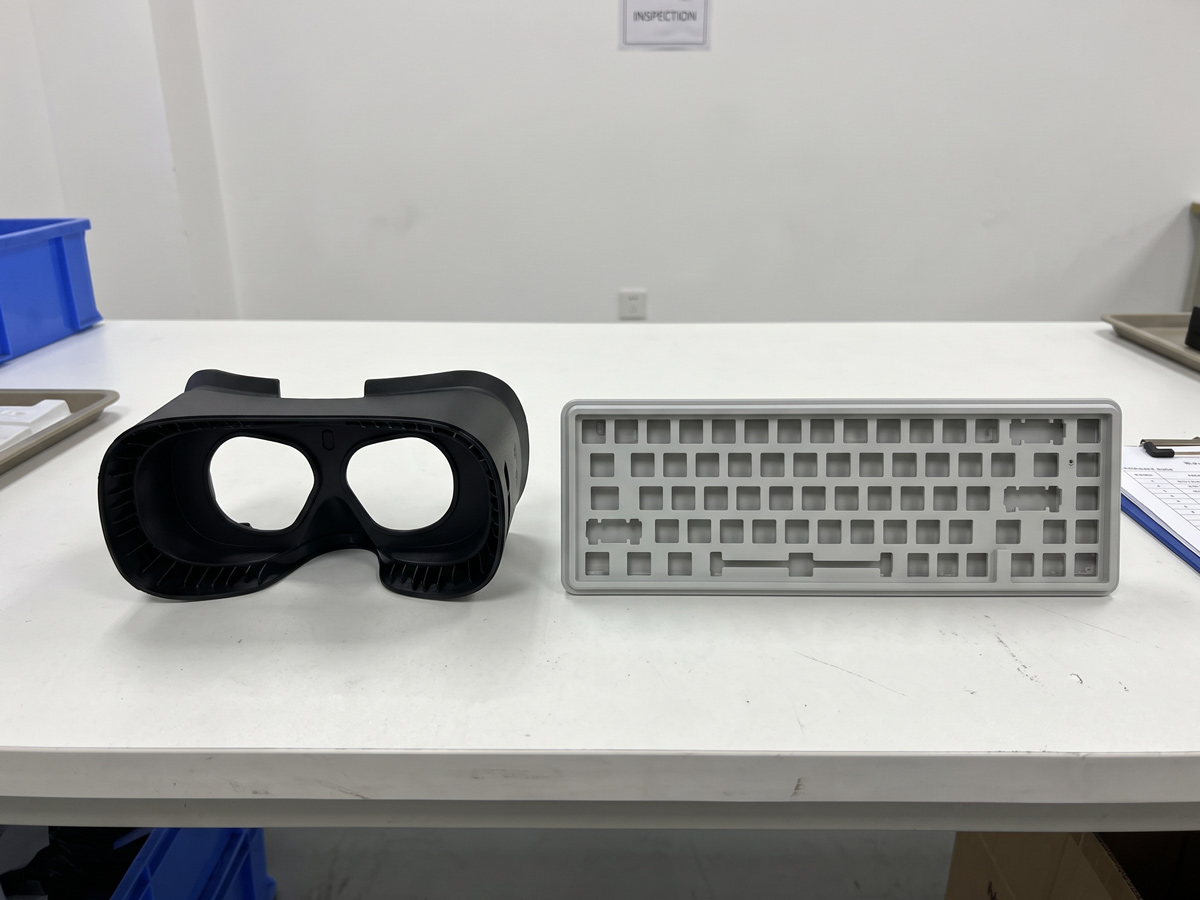
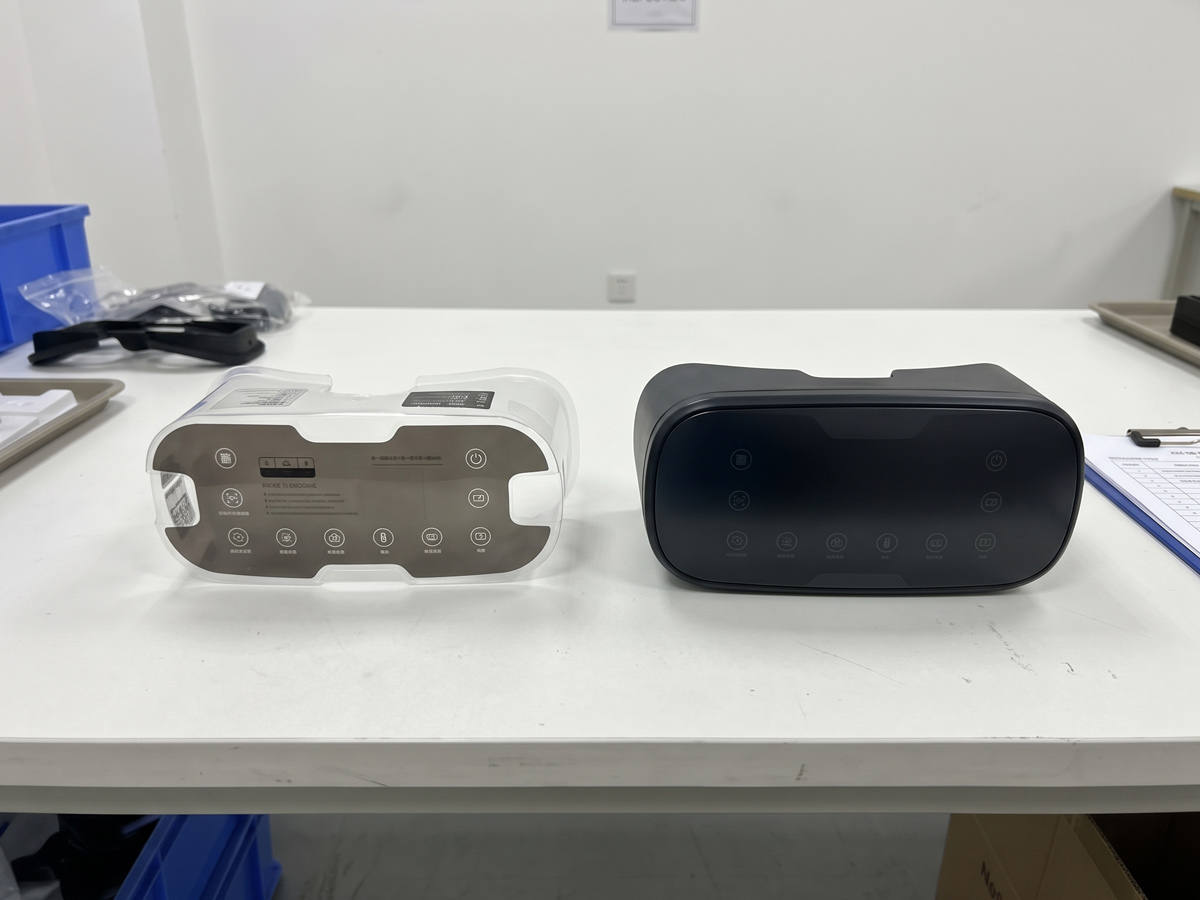
Design & Engineering Challenge: Balancing ultra-lightweight headwear ergonomics with rigid optical lens alignment and heat dissipation.
Our Solution: Engineered thin-wall PC/ABS and glass-fiber reinforced structural frames paired with skin-safe LSR (Liquid Silicone Rubber) facial interfaces molded inside our ISO Class 8 cleanroom.
Design & Engineering Challenge: Preventing long-span chassis warpage (bowing) on ultra-slim 68-key and 98-key enclosures while maintaining crisp acoustic damping.
Our Solution: Optimized multi-gate sequential valve gating, precision two-shot PBT/PC keycap molding, and VDI 21 fine matte EDM bezel textures that resist fingerprint oils.
Design & Engineering Challenge: Achieving museum-grade optical clarity, zero flow marks, and shock-absorbing edge bumpers for high-net-worth trading cards and smartphones.
Our Solution: Mirror-polished S136 optical molds (Ra < 0.05 μm), precision TPU overmolding, and magnetic or ultrasonic-weld tongue-and-groove perimeters held to ±0.005mm.
Design & Engineering Challenge: Machining hundreds of micro-perforated air intake louvers without core pin deflection or visible weld lines across cylindrical exteriors.
Our Solution: High-flow UV-stabilized ABS molding with precision slow-feed Wire EDM louver inserts and seamless drop-in assembly for simple capacitive touch PCBA modules.
Next-Generation Industrial Design Trends: GRS Recycled Resins and IM-3D-E
Industrial design for consumer and commercial hardware is undergoing two structural shifts that directly impact material selection and mold architecture:
- Circular Design & GRS-Certified Recycled Polymers: Western retail buyers and regulatory frameworks are rapidly mandating verifiable recycled content across consumer accessories (Source: Plastics Europe). Designing with Post-Consumer Recycled (PCR) polycarbonate, ABS, or TPU requires upfront DFM adjustments, as recycled resins often exhibit slightly wider melt-flow index (MFI) tolerances and subtle color shifts. Having officially achieved GRS 4.0 certification (Global Recycled Standard) alongside ISO 14001 and RoHS compliance, YG TECH helps designers specify PCR resin blends and micro-textured VDI surfaces that turn eco-friendly materials into a tactile brand advantage.
- Smart Structural Integration via IM-3D-E & IMD: Instead of designing bulky multi-part enclosures screwed together over complex wiring harnesses, modern accessories utilize IM-3D-E (In-Mold 3D Electronics) and IMD (In-Mold Decoration). By encapsulating capacitive touch films, LED light guides, NFC antennas, or simple PCBA sub-assemblies directly into the thermoplastic wall during the injection cycle, designers can reduce part thickness by up to 40% while achieving IP67/IP68 dust and water resistance.
Share your Rhino, SolidWorks, or STEP files under a binding upfront NDA. Our engineers will evaluate parting lines, draft angles, and MUD rapid tooling options within 24–48 hours.
How to Choose the Right Industrial Design & Manufacturing Partner
When launching a custom plastic product, hardware founders and sourcing managers typically face a fork in the road: hire a standalone boutique industrial design agency, or partner with an vertically integrated design-and-manufacturing specialist like YG TECH. Evaluating how each model handles engineering accountability, IP security, and cash flow reveals why integrated execution reduces time-to-market:
| Evaluation Criterion | Standalone Industrial Design Studio | YG TECH (Integrated ID + DFM + Molding Factory) |
|---|---|---|
| DFM & Tooling Feasibility | Focuses on visual renders; often requires expensive CAD rework once sent to a mold shop. | Co-engineered by industrial designers and senior mold makers; holds ±0.01mm standard mold tolerances. |
| Bridge-to-Market Speed | Hands off files and exits; client must source and vet external prototype and tooling vendors. | In-house CNC/3D printing + MUD Rapid Tooling (-30% mold cost, fastest 10-day T0 samples). |
| Production Infrastructure | Zero manufacturing assets; no control over resin lot quality or press scheduling. | 130+ injection machines (50T–800T), ISO Class 8 cleanroom, PPS/LSR/PC/TPU mass-production pedigree. |
| Compliance & Retail Audits | Not applicable at studio level. | ISO 9001 / 14001 / 13485, RoHS, GRS 4.0 certified; passed Amazon and Walmart factory audits. |
| IP Protection & Commercial Terms | High hourly retainer fees; no downstream tooling warranty. | Upfront NDA, 100% client mold ownership upon full payment, 1,000 pcs MOQ, EXW/DDP, flexible Net 30 terms. |
5 Non-Negotiable Checkpoints Before Signing With a Partner
- 1. Upfront NDA & Unconditional Mold Title: Never share native 3D assemblies without a signed Non-Disclosure Agreement. Ensure your contract explicitly guarantees that 100% of the physical mold ownership transfers to you upon final payment—with zero hostage fees if you ever relocate the tool.
- 2. Specialty Polymer & Cleanroom Depth: Verify that the factory has proven experience molding high-temperature engineering resins like PPS, optical polycarbonate, and liquid silicone inside an ISO Class 8 cleanroom so cosmetic surfaces remain free of black specks.
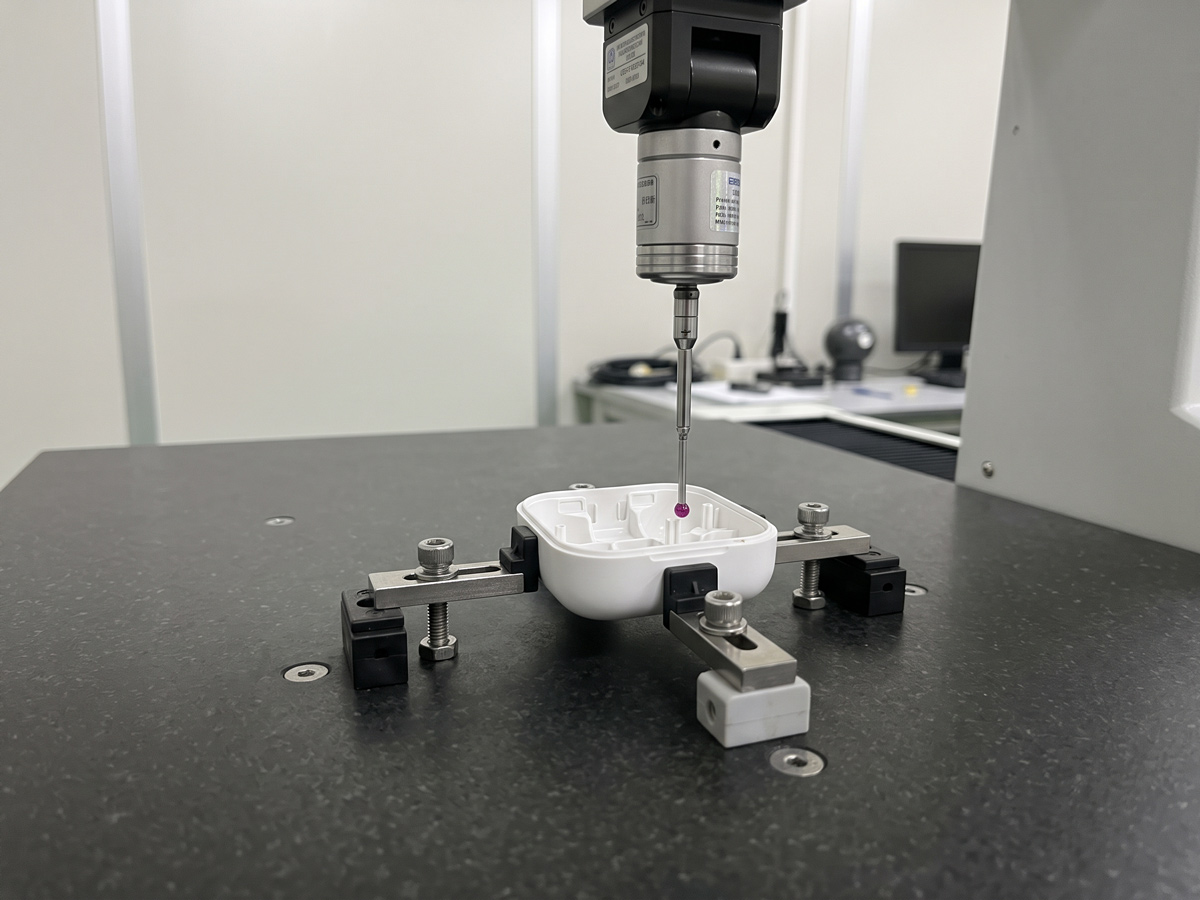
- 3. Closed-Loop Quality Accountability: Ask how the team resolves dimensional or cosmetic defects during pilot runs. At YG TECH, we reject the lazy habit of blindly shipping replacement parts; instead, we execute root-cause metrology traceability (via CMM and 2.5D optical vision) and collaborative steel-safe mold adjustments until the root issue is permanently closed.
- 4. Startup-Friendly Order Agility: Avoid rigid tier-1 conglomerates that demand 50,000-unit commitments. Our 1,000-piece standard MOQ, paired with EXW or door-to-door DDP logistics and adaptable payment options (100% upfront for rapid prototypes, 50% deposit for initial runs, or Net 30 credit terms for qualified recurring partners), protects your working capital.
- 5. End-to-End Finishing & Simple PCBA Sub-Assembly: For $30+ retail accessories, consolidating molding, ultrasonic welding, pad printing, laser etching, simple PCBA drop-in assembly, and retail packaging at a single audited facility eliminates multi-vendor tolerance stack-up.
Turn Your Industrial Design Into Production-Ready Tooling
Whether you have an early Rhino concept that needs DFM refinement or a locked SolidWorks assembly ready for 10-day MUD rapid tooling, our engineering team is ready to support your launch.
Ideal for hardware startups and SMEs validating ergonomics, CMF textures, and snap-fit mechanics with 30% lower upfront tooling investment.
Submit 3D Files for DFM & MUD Quote →Scale from 1,000-unit MOQs to 500,000+ shots in our ISO Class 8 cleanroom and 50T–800T molding bays with 100% client mold ownership.
Speak With a Senior Project Engineer →